How to Tram a Vertical Milling Machine Head?

Time:2026-10-28 Author:Amelia
0%

A vertical milling head can look square while cutting noticeably out of tram. The evidence appears on the workpiece: one side of a facing cut shines wider, cutter marks vary, and edge dimensions drift. Learning how to tram a vertical milling machine head helps prevent these errors before they become expensive parts. It also builds a stronger understanding of machine alignment, tooling, and measurement.

Tom Lipton, a respected machinist and manufacturing educator, often stresses, “The setup is the work.” That principle fits this task perfectly. Tramming is not merely loosening bolts and tapping the head into position. It requires a clean table, a reliable tram indicator, controlled adjustments, and patience. Even a thin chip under the head or indicator base can create a false reading. Small details matter.

This guide will explain how to check the head from side to side and front to back. It will also cover indicator movement, adjustment methods, tightening sequence, and final verification. A dial test indicator, a rigid holder, and a clean reference surface are essential. Do not trust the first reading. Check it twice.

The process may feel slower than expected. That is normal. A perfect reading is not always practical on an older machine, either. The goal is repeatable accuracy within the work required. After adjustment, a light test cut should confirm the result. If the cut still varies, revisit the setup instead of blaming the cutter. Mistakes happen. Careful measurement exposes them.
How to Tram a Vertical Milling Machine Head?

Understanding Vertical Milling Machine Head Tramming

How to Tram a Vertical Milling Machine Head?

Understanding Vertical Milling Machine Head Tramming

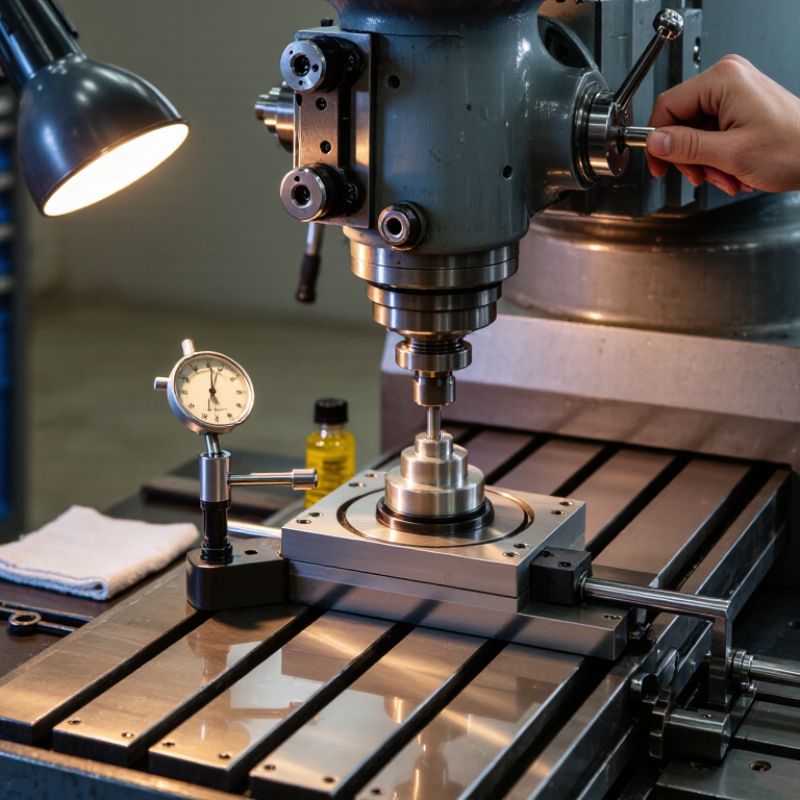
Tramming aligns the spindle axis square with the milling table. It controls cutter contact, surface finish, and insert wear during face milling. Clean surfaces first. Chips beneath the head or indicator can create a false reading. I wipe the table, spindle taper, and indicator arm before measuring.

Mount a dial test indicator in the spindle and sweep a known table distance. A 0.05 mm height difference across 150 mm equals approximately 0.019 degrees of angular error. That small angle can leave visible steps on a wide face. ISO 230-2:2014 emphasizes repeatability and measurement conditions when evaluating machine-tool accuracy. Therefore, record the indicator readings, spindle position, and environmental conditions. Measure, do not guess.

Loosen the head only enough for controlled adjustment. Tap it gently, then tighten the bolts in stages. Recheck the sweep after every adjustment. The National Institute of Standards and Technology highlights traceable measurement and uncertainty control in manufacturing metrology. That principle matters here: indicator resolution does not guarantee actual accuracy. I usually target near-zero variation, but real machines may require a practical tolerance based on their condition and workpiece size. My first attempt is rarely perfect. Tightening can shift the head again. A final sweep under normal clamping pressure exposes that mistake.

Preparing the Machine, Tools, and Measuring Equipment

Preparing a vertical milling machine head begins with a clean, stable reference surface. Remove chips from the table, ways, and spindle nose. Even a thin chip can create a false tram reading.

Gather a rigid test bar, a calibrated dial test indicator, a wrench set, and a torque wrench. Check the indicator for smooth movement before mounting it. Use a bar long enough to reveal angular error, but not so long that it bends. A 300 mm sweep can magnify small alignment problems. Record front, rear, left, and right readings in a simple worksheet. ISO 230-2 emphasizes repeatable measurement conditions during machine tool accuracy testing. Keep the spindle warm for several minutes, because temperature can change readings.

Calibration matters. The NIST Technical Note 1297 explains that an expanded uncertainty commonly uses coverage factor k = 2, representing roughly 95% confidence. Therefore, do not treat a 0.01 mm difference as absolute truth without considering instrument resolution and setup variation.

Repeat each reading at least three times. Small differences may come from operator pressure, loose mounting, or an uneven table.

Keep the head bolts lightly secured while making adjustments. Tighten them gradually, then measure again. I have found that rushing this step creates misleadingly perfect results. That is worth questioning. A final check with a machinist’s square can expose remaining side-to-side error, especially when the indicator setup hides it.

Aligning the Head Side to Side

How to Tram a Vertical Milling Machine Head?

Aligning the Head Side to Side

Side-to-side alignment affects slot width, shoulder accuracy, and surface finish. I begin with a clean table and a spindle that turns freely. Remove chips from the table, spindle taper, and indicator mount. Small debris can create a surprisingly large error.

I place a dial indicator in the spindle and position its tip near the table’s front edge. The indicator should remain stable during rotation. I rotate the spindle by hand and compare readings at the left and right sides. A difference shows that the head is tilted sideways. Do not adjust it yet. Check the indicator, table cleanliness, and spindle movement first.

After loosening the head’s securing bolts slightly, I make a small correction with the built-in adjustment mechanism. Tiny movements matter. I sweep both sides again and record the readings. If the left side reads high, I adjust gradually in the opposite direction. The correct direction can vary with the machine design, so I never force the head. Once the readings are close, I tighten the bolts in stages and recheck the alignment. This step often changes the result.

I aim for a minimal difference suitable for the work required. Precision depends on the machine, indicator, and machining conditions. I once trusted the first reading too quickly. That assumption was wrong. Rechecking after tightening prevented an uneven shoulder and saved a workpiece. Wear, temperature, and table condition can also influence the final measurement.

How to Tram a Vertical Milling Machine Head? - Aligning the Head Side to Side
Step Data Dimension Recommended Value or Condition Practical Procedure and Technical Notes
1 Machine preparation Clean, dry, and stable Clean the table, spindle taper, toolholder, drawbar contact surfaces, and the indicator mounting point. Remove chips, burrs, and oil films that could affect alignment.
2 Machine temperature Thermally stabilized Allow the machine to reach a consistent operating temperature before final measurement. Thermal changes can alter readings as the spindle, head, and table expand.
3 Required measuring tools Dial test indicator, rigid holder, hex keys, torque wrench Use a rigid indicator setup with the contact point approximately perpendicular to the measured surface. A dial test indicator is commonly used because it responds well to small angular changes.
4 Indicator sweep radius 100–150 mm (4–6 in) Mount the indicator so its tip can reach both the left and right sides of a clean table surface or a precision parallel. A larger sweep radius makes small angular errors easier to detect.
5 Spindle condition Stopped and secured Do not rotate the spindle under power during setup. Lock or secure machine axes as appropriate, while keeping the table movement controlled and repeatable.
6 Initial indicator setup Light, consistent contact Touch the indicator tip to the table or reference surface with only enough preload to maintain reliable contact. Excessive preload can deflect the indicator arm or the mounting arrangement.
7 Reference position Zero at one side Rotate the spindle by hand to place the indicator at the left side of the sweep. Set the dial to zero without moving the table or changing the indicator angle.
8 Opposite-side reading Record the right-side deviation Rotate the spindle by hand through 180 degrees to place the indicator at the right side. Record the reading without changing the indicator position or table height.
9 Side-to-side error Difference between left and right readings If the left reading is zero and the right reading is +0.04 mm, the total side-to-side difference is 0.04 mm. Repeat the sweep to confirm the result and rule out dirt or indicator binding.
10 Angular error estimate Angle ≈ arctangent(error ÷ sweep diameter) For a 200 mm sweep diameter and 0.04 mm difference, the angular error is approximately 0.011°: arctan(0.04 ÷ 200). This estimate assumes the measured surface is flat and the indicator setup is rigid.
11 Typical alignment target About 0.02–0.05 mm over 200 mm A practical target for general milling work is often within 0.02–0.05 mm over a 200 mm sweep. The required tolerance depends on the workpiece, cutter diameter, surface-finish requirements, and machine condition.
12 Head adjustment Small, controlled movement Loosen the head swivel or side-to-side adjustment fasteners only enough to permit controlled movement. Follow the machine’s service instructions and support the head if required by its design.
13 Adjustment direction Move the low side toward alignment Use the indicator readings to determine which side of the head is high or low. Make very small corrections, then lightly snug the fasteners before measuring again.
14 Measurement repeatability At least two confirming sweeps After each adjustment, return to the same reference position and repeat the full left-to-right sweep. Consistent readings are more important than a single low reading.
15 Fastener tightening Use the specified tightening sequence and torque Tighten the head fasteners gradually and evenly. If the manufacturer’s torque specification is available, use it; otherwise, avoid excessive force that could shift the head or damage threads.
16 Final verification Recheck after full tightening Repeat the indicator sweep after all fasteners are fully tightened. The head can move slightly during tightening, so the final reading must be taken in the secured condition.
17 Measurement limitations Reference surface must be clean and suitable Table wear, dents, burrs, contamination, spindle runout, loose tooling, and indicator flex can produce misleading results. Check these conditions before making major head adjustments.
18 Safety requirement Power isolated during adjustment Stop the machine and isolate power before reaching near the head, loosening adjustment fasteners, or changing the indicator setup. Keep hands clear of pinch points and support heavy components safely.

Aligning the Head Front to Back

How to Tram a Vertical Milling Machine Head?

Aligning the Head Front to Back

Front-to-back tram controls how the spindle meets the workpiece along the table’s length. Begin with a clean table, a sharp indicator, and a warm machine. Remove chips from the column, head, and mounting surfaces. A small chip can create a surprisingly large angular error.

Install a test bar or indicator in the spindle. Sweep a fixed diameter near the table, then rotate the spindle by hand. Record the front and rear readings at equal distances. For example, a 0.01 mm difference across 150 mm represents about 0.0038 degrees, or nearly 14 arcseconds. That error may leave visible steps during face milling. ISO 230-2:2014 emphasizes repeatability and systematic accuracy, so repeat the sweep before adjusting anything. Do not chase noise.

Loosen the head bolts only enough for controlled movement. Adjust the front-to-back angle in tiny increments, often using gentle pressure and a soft mallet. Recheck both sides after every change. Tightening can pull the head away from the dialed position. NIST Technical Note 1297 also stresses measurement uncertainty; indicator resolution is not the same as machine accuracy. Keep the spindle, table, and indicator contact clean. Keep the table still.

A final sweep should show nearly equal readings within the tolerance required by the job. I usually make one extra check after tightening, because the first “perfect” setting is sometimes not perfect. Temperature, loose hardware, and table wear can change the result. Record the readings, correction direction, and final condition for the next setup.

Verifying Tram Accuracy and Making Final Adjustments

Verifying tram accuracy starts with a clean table, spindle, and test bar. Remove chips from every contact surface. Install a rigid dial indicator holder, then sweep a 100–150 mm circle across the table. Record readings at the front, rear, left, and right positions. Do not trust one pass. Thermal drift, dirt, and uneven tightening can change the result. ISO 230-2:2014 recommends repeatable measurement methods for machine-tool accuracy, so repeat the sweep at least three times.

Compare the highest and lowest readings, then check the machine’s specified tolerance. NIST Technical Note 1297 advises reporting measurement uncertainty with an expanded uncertainty, commonly using k=2 for approximately 95% coverage. That matters when the measured difference is only a few micrometres. My first reading is rarely perfect. That is normal. Allow the spindle and machine to reach a stable temperature before judging the result.

For final adjustments, loosen the head bolts only enough to permit controlled movement. Tap gently with a soft mallet, then retighten in a cross pattern. Sweep the indicator again after each adjustment. Watch for bolt tightening that pulls the head out of tram. A practical target is the tightest value permitted by the machine’s service specification, not an impressive number copied from another mill. Record the initial reading, adjustment direction, final reading, temperature, and indicator resolution. ISO 230-1 also emphasizes defined test conditions, yet operators sometimes overlook them. I have done that myself. The record exposes whether the adjustment truly improved accuracy.

How to Tram a Vertical Milling Machine Head

Verifying Tram Accuracy and Making Final Adjustments

The chart shows representative dial-indicator readings taken at four positions during a 300 mm sweep under the spindle. Readings closer to zero indicate better alignment. After loosening the head, making small angular corrections, and retightening the bolts, the final readings are substantially closer to zero.

FAQS

What does tramming a vertical milling head achieve?

Tramming makes the spindle axis square with the milling table. It improves cutter contact and surface finish. It can also reduce uneven insert wear. Small errors matter.

What should be cleaned before measuring?

Clean the table, ways, spindle taper, and head mounting surfaces. Remove every visible chip. Even a thin chip can distort the reading. Cleanliness is part of accuracy.

Which tools are useful for head tramming?

Use a rigid test bar, dial test indicator, wrench set, and torque wrench. A machinist’s square can check side-to-side alignment. The bar must resist bending. A 300-millimeter sweep reveals small errors clearly.

How should the indicator readings be recorded?

Record front, rear, left, and right readings. Note the spindle position and machine temperature. Repeat each measurement at least three times. Write down the correction direction.

How do you align the head from front to back?

Mount the indicator or test bar in the spindle. Sweep equal distances at the front and rear. Rotate the spindle by hand. Adjust the head in tiny increments, then measure again.

How much error can affect a milled surface?

A 0.05-millimeter difference across 150 millimeters creates about 0.019 degrees of angular error. That small angle may leave visible steps. A 0.01-millimeter difference can also matter on wide surfaces.

How should the head bolts be adjusted?

Loosen the bolts only enough for controlled movement. Tap the head gently with a soft mallet. Tighten the bolts in stages. Recheck after every adjustment.

Why can a perfect indicator reading still be misleading?

Indicator resolution does not guarantee actual machine accuracy. Temperature, table wear, loose hardware, and mounting pressure affect results. My first setting is rarely perfect. That deserves skepticism.

What is the final check after tramming?

Sweep the indicator again under normal clamping pressure. Confirm nearly equal readings within the job’s tolerance. Check the result with a square when possible. Record the final condition.

Conclusion

This guide explains how to tram a vertical milling machine head so the spindle is properly aligned with the table. It begins by describing why accurate head tramming matters for consistent cuts, square surfaces, and predictable tool performance. The process includes preparing the machine, cleaning the mating surfaces, gathering suitable measuring tools, and securing the work area before making any adjustments.

The head is then checked from side to side and from front to back using a reliable reference surface and a sensitive indicator. Small, controlled adjustments are made until the readings are consistent across the measurement path. Finally, the alignment is verified through repeated checks, with attention given to tightening fasteners without disturbing the setting. This systematic approach helps ensure accurate results and establishes a repeatable method for future inspections and adjustments.
Amelia

Amelia

Amelia is a seasoned marketing professional with a wealth of expertise in our company’s core offerings. With an unwavering passion for driving growth and innovation, she plays a pivotal role in shaping our marketing strategies and enhancing brand visibility. A key aspect of her responsibilities......