How to Tell If a CNC Spindle Bearing Is Failing?

Time:2026-11-18 Author:Charlotte
0%

A CNC spindle bearing rarely fails without warning, but its early signals can be subtle. A faint high-pitched whine may appear during a familiar toolpath. Vibration can show up as chatter marks, poor surface finish, or unexpected tool wear. Heat may collect around the spindle nose, even when the machine sounds normal. These clues matter most when compared with the machine’s usual behavior under similar speed, load, and ambient conditions. One warm reading alone proves little.

So, what are the signs that a cnc spindle bearing is failing? Common indicators include rising vibration, unusual noise, excess temperature, spindle runout, and worsening part quality. A technician can check these signs with suitable instruments, such as a vibration analyzer, temperature probe, and dial indicator. Keep the test setup consistent, and record readings over time. A single measurement can mislead. So can a rushed diagnosis.

This guide explains what to observe, how to separate bearing symptoms from issues such as imbalance or tool-holder problems, and when to stop machining for inspection. Follow the machine builder’s maintenance guidance, and avoid treating a sound or temperature reading as a definitive diagnosis. That distinction is easy to miss. I have seen troubleshooting become less clear when people replace parts before checking the basics. Careful records and qualified inspection usually provide a more dependable path to a repair decision.
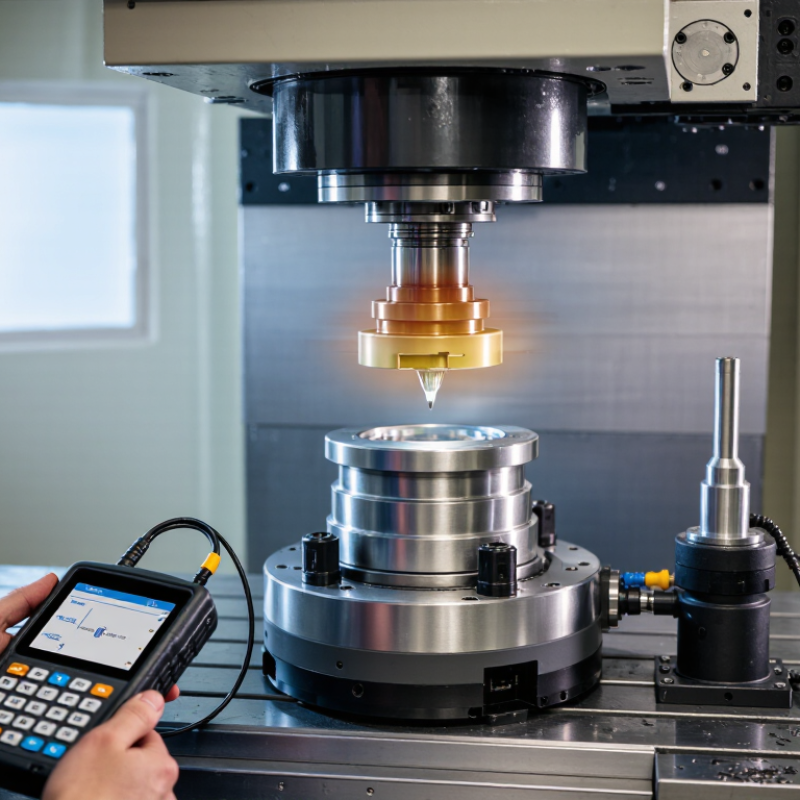
How to Tell If a CNC Spindle Bearing Is Failing?

Recognize Failure Symptoms: Heat, Noise, Vibration, and Runout

A failing CNC spindle bearing often reveals itself through changes that build over time. Heat is one clue: after a consistent warm-up, compare the spindle housing temperature with its usual reading. A new hot spot or steadily rising temperature deserves attention. Check that coolant flow, lubrication, and cutting conditions have not changed; these can also affect heat. Temperature alone is not a diagnosis.

Listen for a new whine, rumble, or periodic grinding sound, especially at a repeatable spindle speed. Note when it starts and whether it changes under load. Then compare vibration readings with the machine’s baseline, using the same sensor position and operating conditions. A rough sound alone can fool you. Tool imbalance, a damaged holder, or a loose fixture may produce similar symptoms, and it is easy to blame the bearing too quickly.

Runout offers another useful clue. With the spindle stopped and safely accessible, use a suitable dial indicator to check a clean, correctly seated test bar; follow the machine maker’s procedure and compare results with its limits. Increasing runout, paired with heat or vibration, raises concern, but contamination or poor seating can distort the reading. Record measurements rather than relying on memory. If symptoms worsen, stop cutting and have a qualified technician inspect the spindle before further operation.

Classify Bearing Damage Using ISO 15243 Failure Categories

How to Tell If a CNC Spindle Bearing Is Failing?

Classify Bearing Damage Using ISO 15243 Failure Categories

A rising spindle temperature, rough sound, or vibration can signal trouble, but none identifies the cause alone. ISO 15243 classifies rolling-bearing damage into fatigue, wear, corrosion, electrical erosion, plastic deformation, and fracture or cracking. These categories help turn inspection clues into a more disciplined diagnosis. Not proof.

Fatigue may appear as flaking or small pits on raceways, often after repeated contact stress. Wear can leave polished tracks, scoring, or material loss; check for abrasive particles and inadequate lubrication.

Corrosion may show as reddish-brown marks or etched surfaces, especially after moisture exposure. Electrical erosion can create fine fluting or darkened, crater-like marks.

Plastic deformation often leaves dents where rolling elements contacted the raceway, sometimes after impact or excessive load.

Fractures and cracks need careful attention. Their location and direction can offer clues about overload, poor fits, or mounting damage, but inspection alone may not establish the root cause. A clean-looking bearing can still have internal damage.

It is tempting to blame every high-pitched whine on fatigue; that shortcut can mislead. Record vibration, temperature, lubricant condition, operating speed, and preload history, then compare these findings with the bearing’s physical marks. Preserve the failed parts for examination rather than wiping away evidence.

Track Vibration at 1× Speed and Bearing-Defect Frequencies

A failing CNC spindle bearing may produce a faint whine before noticeable heat or looseness appears. Track vibration at the spindle housing with a sensor mounted firmly in the same location each time. Record readings at idle and at several operating speeds, noting the exact RPM and tool condition. The 1× speed component matches shaft rotation, so a rising peak can point to imbalance, misalignment, or a developing mechanical change. It does not identify the cause by itself. Compare readings over time, rather than relying on one measurement.

Tips: Keep the sensor position consistent. Log RPM, load, and temperature. Avoid comparing data from different setups.

Bearing defects can generate vibration at characteristic frequencies linked to the rolling elements, cage, and raceways. These frequencies may appear above 1× speed and can become clearer in a high-frequency spectrum or envelope analysis. Look for repeatable peaks and sidebands, not just a single tall line. A loose tool, changing cutting load, or poor sensor contact can distort the picture. I would treat an unusual reading as a prompt to inspect, not proof of bearing failure. Confirm it with noise, temperature, and runout checks before planning service.

Compare Runout and Temperature with the Spindle Maker’s Limits

A spindle bearing rarely announces failure with one dramatic symptom. Compare measured runout and temperature with the spindle maker’s limits, not generic numbers copied from another machine. ISO 230-7:2015 describes methods for measuring rotating-axis error motion, including spindle error motion. It does not set one pass-or-fail limit for every spindle. The maker’s specification is the reference.

Measure runout with a clean, known-good test bar, consistent gauge position, and the same spindle speed each time. Record the reading before and after warm-up. A rising value matters more than one isolated measurement. Small setup differences can mislead. That is easy to miss. For temperature, use the same sensor location and note ambient temperature, warm-up time, speed, and load. Compare readings with the maker’s stated operating range and watch for a repeatable upward trend.

ISO 281:2007 explains that basic bearing rating life calculations use a 90% reliability basis under stated operating assumptions. That figure is not a field diagnosis or a guarantee for an individual spindle. If runout or temperature exceeds the spindle maker’s limit, stop and verify the measurement setup before returning the machine to production. I would also check for toolholder contamination and unusual vibration; those checks are useful, but they do not replace the specified limits. A trend log helps, though imperfect notes can still hide a developing change.

How to Tell If a CNC Spindle Bearing Is Failing? - Compare Runout and Temperature with the Spindle Maker’s Limits

Note: The readings and limits below are hypothetical examples for showing how to compare measurements. They are not universal acceptance limits. Use the spindle maker’s specifications and measurement procedure for the specific spindle.

Example condition Taper runout (µm TIR) Example maker limit (µm TIR) Housing temperature rise above stabilized idle (°C) Example maker limit for rise (°C) What the comparison suggests
Stable reference check 2 5 12 25 Both readings are below the example limits. Record them as a baseline and trend future checks under comparable conditions.
Near-limit readings 4 5 20 25 Still within the example limits, but close enough to warrant a repeat measurement and closer trend monitoring.
Both readings exceed limits 7 5 31 25 A repeatable exceedance in both measurements is a strong reason to stop and follow the maker’s inspection or service guidance.
Temperature exceeds limit; runout does not 3 5 29 25 Check the specified warm-up and test conditions, lubrication, cooling, load, and temperature measurement location. Normal runout alone does not rule out a problem.
Runout exceeds limit; temperature does not 8 5 14 25 Repeat the test using the maker’s method. Check the gauge setup, taper cleanliness, and test arbor or toolholder before concluding that the spindle bearings are failing.

For a meaningful comparison, measure runout at the specified location with a suitable indicator and consistent setup. Measure temperature at the specified housing location after the prescribed warm-up or operating cycle, and compare it with the maker’s limit under the same conditions.

Estimate Bearing Rating Life with ISO 281 L10 at 90% Reliability

A CNC spindle bearing can sound rough before it becomes visibly damaged. Rising temperature, a new whine, or vibration at a familiar speed deserve attention. But symptoms alone cannot tell you how much useful life remains. ISO 281 provides a rating-life estimate, not a failure date.

The basic L10 life represents the life that 90% of a sufficiently large group of identical bearings are expected to reach or exceed under stated conditions. Calculate it as L10 = (C/P)p million revolutions, where C is the bearing’s basic dynamic load rating and P is its equivalent dynamic load. Use p = 3 for ball bearings and 10/3 for roller bearings. To estimate hours, multiply L10 by one million, then divide by 60 times spindle speed in rpm. Check the units carefully.

A clean calculation can still be misleading. Spindle preload, heat, lubrication, contamination, and changing cutting forces can alter real operating conditions. A bearing may run quietly today and deteriorate quickly after a lubrication problem. Conversely, some noise comes from another component. Compare temperature and vibration trends with the machine’s baseline, and verify loads and speed before trusting the estimate. That estimate can be wrong. ISO 281 L10 is a planning tool, not a substitute for inspection or condition monitoring.

FAQS

What are common signs of a failing CNC spindle bearing?

Watch for rising housing temperature, new whine or rumble, increased vibration, and growing runout. One sign alone proves little.

How should I check spindle temperature?

Measure the housing after the same warm-up each time. Note new hot spots or a steady rise. Check coolant, lubrication, and cutting conditions too.

Can a new grinding sound confirm bearing damage?

No. A loose fixture, damaged tool holder, or tool imbalance can sound similar. Note the speed and load when the noise begins.

How can I track spindle vibration consistently?

Mount the sensor firmly in the same spot. Record readings at idle and several speeds, including RPM, load, and tool condition. Keep the setup consistent.

What does a rising 1× vibration peak mean?

It matches shaft rotation and may indicate imbalance, misalignment, or another mechanical change. It does not identify the cause by itself.

What vibration patterns may suggest bearing defects?

Defect-related peaks can appear above 1× speed, sometimes with sidebands. High-frequency spectrum or envelope analysis may make them clearer. Check for repeatable patterns.

How should I check spindle runout?

With the spindle stopped and safely accessible, check a clean, correctly seated test bar using a suitable dial indicator. Follow the machine procedure and record the result.

What should I do if several symptoms appear together?

Heat, vibration, and increasing runout together raise concern, but readings can still mislead. Stop cutting if symptoms worsen. Arrange a qualified inspection before operating again.

Conclusion

To understand what are the signs that a cnc spindle bearing is failing, watch for rising operating temperatures, unusual whining or grinding noises, increased vibration, and excessive spindle runout. These symptoms may appear gradually or worsen under load, but no single sign confirms bearing failure. Record when each change occurs and compare readings over time to distinguish a developing problem from normal operating variation.

A structured assessment can help identify the cause and urgency. Classify visible or suspected damage using the ISO 15243 failure categories, and analyze vibration at the spindle’s 1× rotational speed and at bearing-defect frequencies. Compare runout and temperature readings with the spindle maker’s specified limits. For maintenance planning, estimate bearing rating life using ISO 281 L10, which represents a 90% reliability basis—not a guarantee that an individual bearing will reach that life.

Charlotte

Charlotte

Charlotte is a seasoned marketing professional with a deep understanding of the company's portfolio and a passion for elevating its presence in the market. With a keen eye for detail and a commitment to excellence, she ensures that our professional blog is regularly updated with insightful articles......